Problem
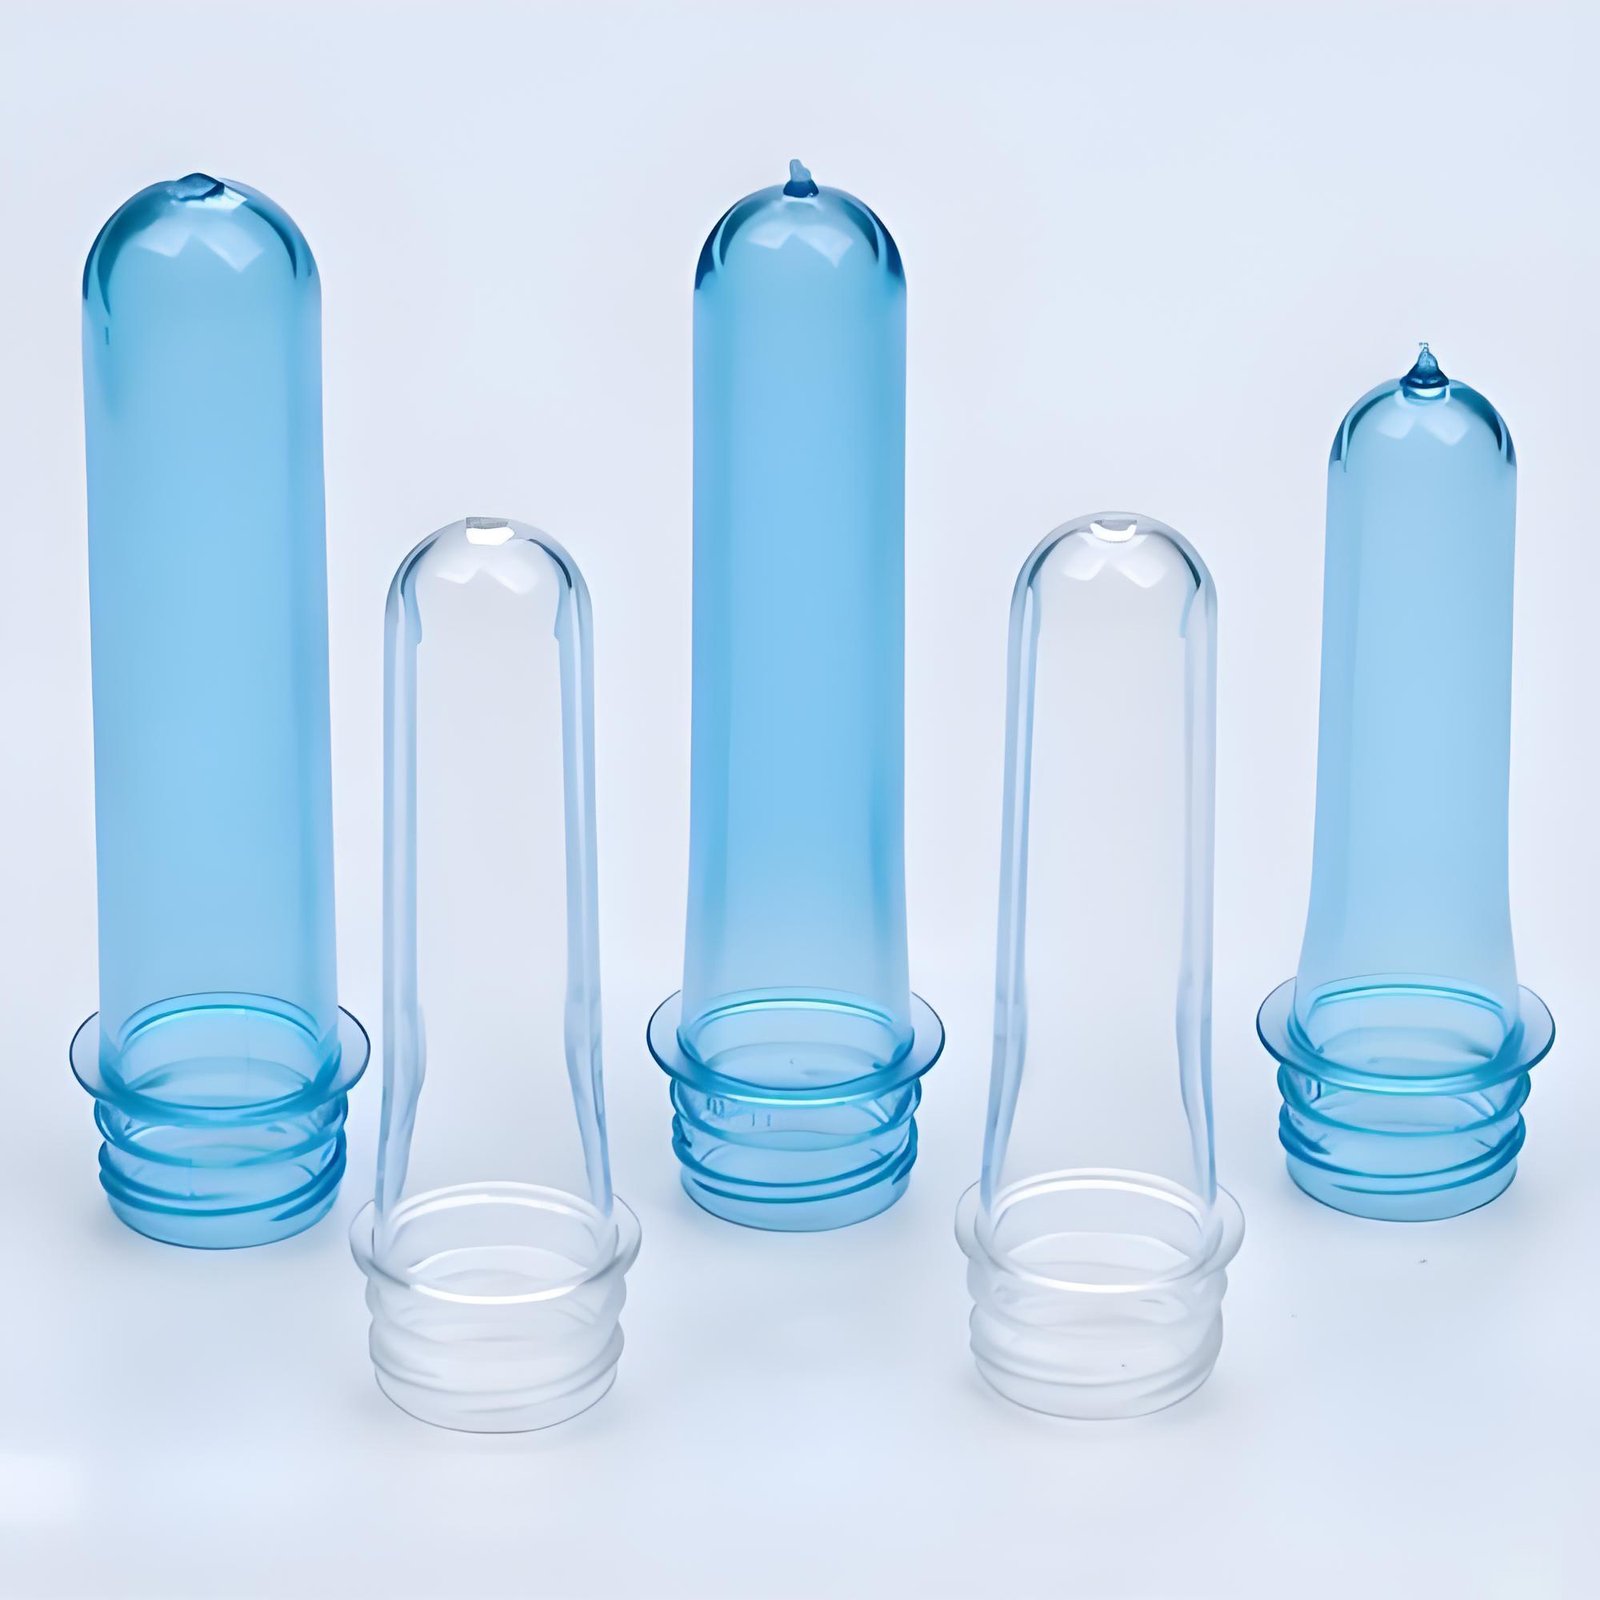
PET preform moulding demands a homogeneous, high-temperature melt delivered at high speed, yet processors often see inconsistent preform wall thickness, gate stringing, drooling and slow cycle times that limit output.
Typical Causes
- 01PET’s high melting point and low melt strength make uniform plasticising difficult on general-purpose screws.
- 02Residual moisture in inadequately dried resin drives hydrolysis and intrinsic-viscosity (IV) loss.
- 03Worn screw flights and barrel bore reduce melt homogeneity and shot-weight repeatability.
- 04Insufficient L/D ratio and compression for PET leave unmelted pellets and temperature gradients.
- 05Poor nozzle shutoff leaves gate vestige and stringing after mould open.
Technical Challenges
- Achieving a uniform melt temperature window without overheating and generating acetaldehyde (AA).
- Maintaining intrinsic viscosity (IV) through controlled residence time and shear.
- Filling multi-cavity preform tools at high speed with consistent shot weight.
- Producing a clean gate break on every cycle to avoid vestige and contamination.
Rootier's Technical Solutions
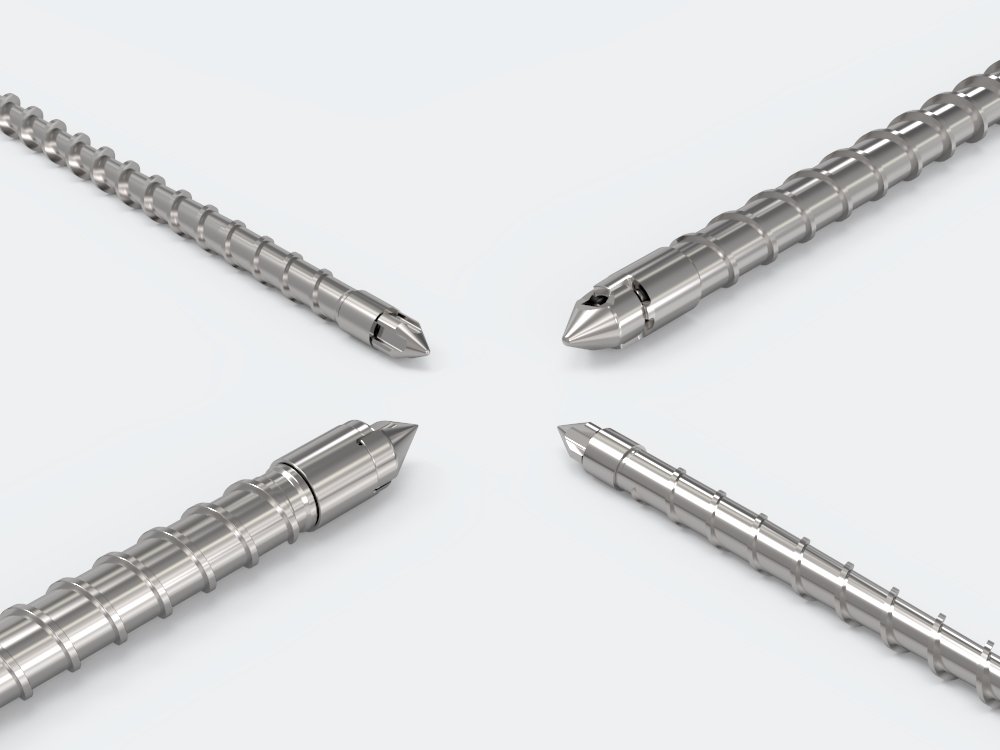
- 01High-L/D (24:1–26:1) barrier screws engineered for PET melting and metering uniformity.
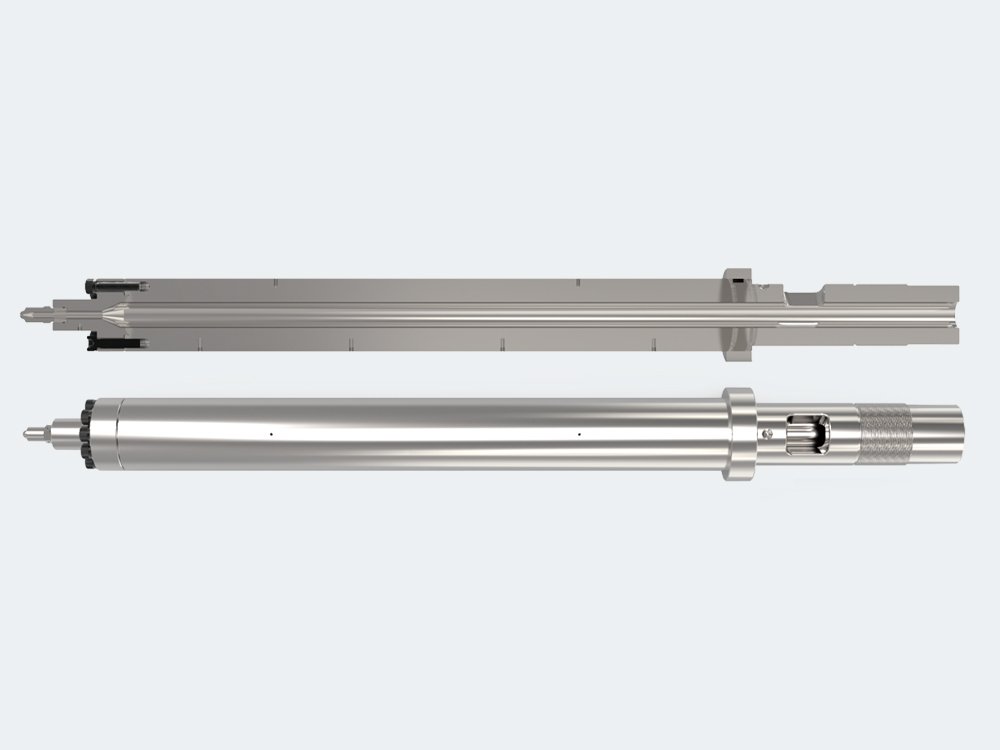
- 02Bimetallic barrels that resist wear from any regrind or catalyst residue.
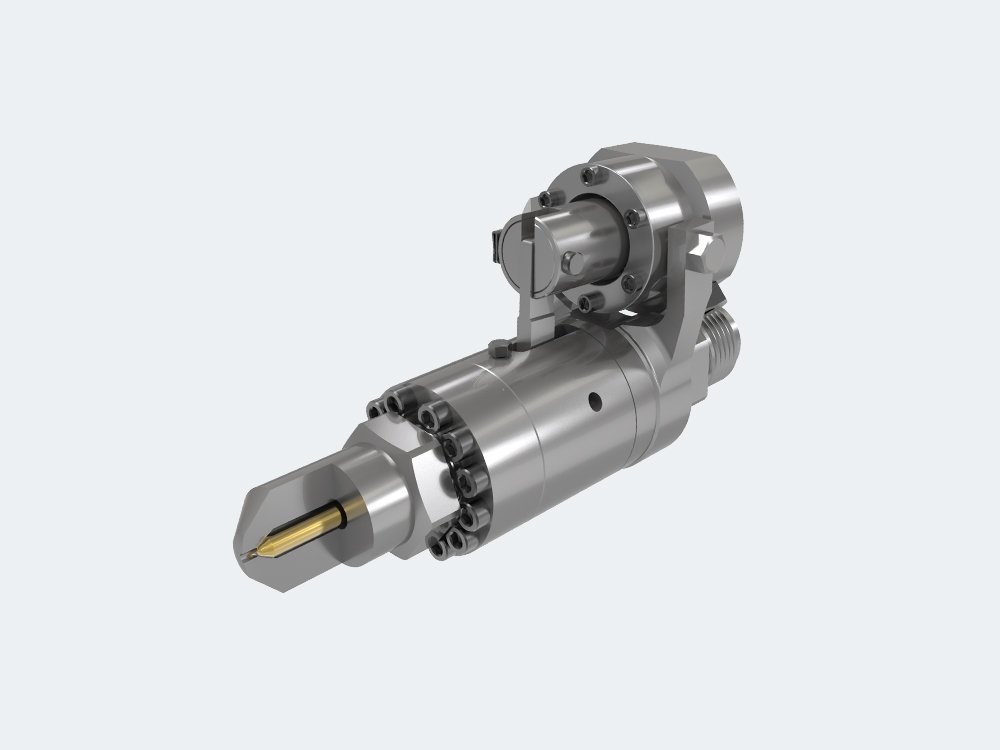
- 03Needle shutoff nozzles for positive, repeatable gate shutoff and clean break.
- 04Optimised compression ratio and metering depth to balance shear and throughput.
- 05Surface treatments (nitriding / PVD) that reduce melt adhesion and shear heat.
Recommended Products
Applications / Materials
Frequently Asked Questions
A high-L/D (24:1–26:1) barrier screw with a properly designed compression and metering section delivers the uniform, high-temperature melt PET needs for consistent preform weight and fast cycling.
A needle shutoff nozzle provides positive, repeatable gate shutoff for a clean break every cycle. Correct decompression and nozzle temperature settings further reduce vestige and stringing.
Control melt temperature and residence time. A low-shear barrier screw and bimetallic barrel that hold tolerance help avoid overheating, which is the main driver of AA generation.