Problem
Crate and pallet moulding uses large shot volumes, high regrind content and often mineral- or glass-filled HDPE/PP, which accelerates wear and causes flash, sink marks and long, inconsistent cycles.
Typical Causes
- 01Large shot weights demand long plasticising time on undersized screws.
- 02Regrind and filler content abrade screw flights and barrel bore rapidly.
- 03Worn barrels leak melt pressure, reducing packing and causing sink.
- 04Inconsistent dosing from worn non-return valves affects part weight.
- 05High clamping forces and long cycles stress plasticising components.
Technical Challenges
- Delivering consistent large-shot weights across heavy tools.
- Resisting wear from regrind, talc and glass-filled grades.
- Controlling warpage and sink in thick structural sections.
- Keeping cycle times stable over long production campaigns.
Rootier's Technical Solutions
- 01Bimetallic barrels with wear-resistant liners for high-throughput runs.
- 02Wear-clad screws (HVOF / tungsten carbide) for regrind and filled HDPE/PP.
- 03High-throughput screw geometries sized to the shot and recovery time.
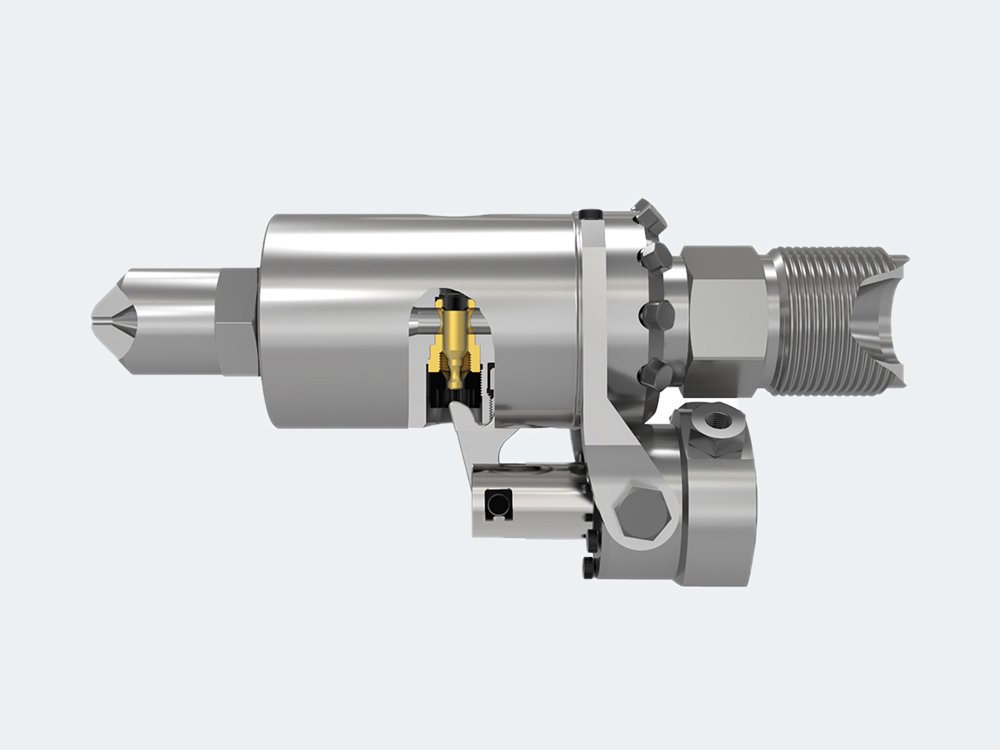
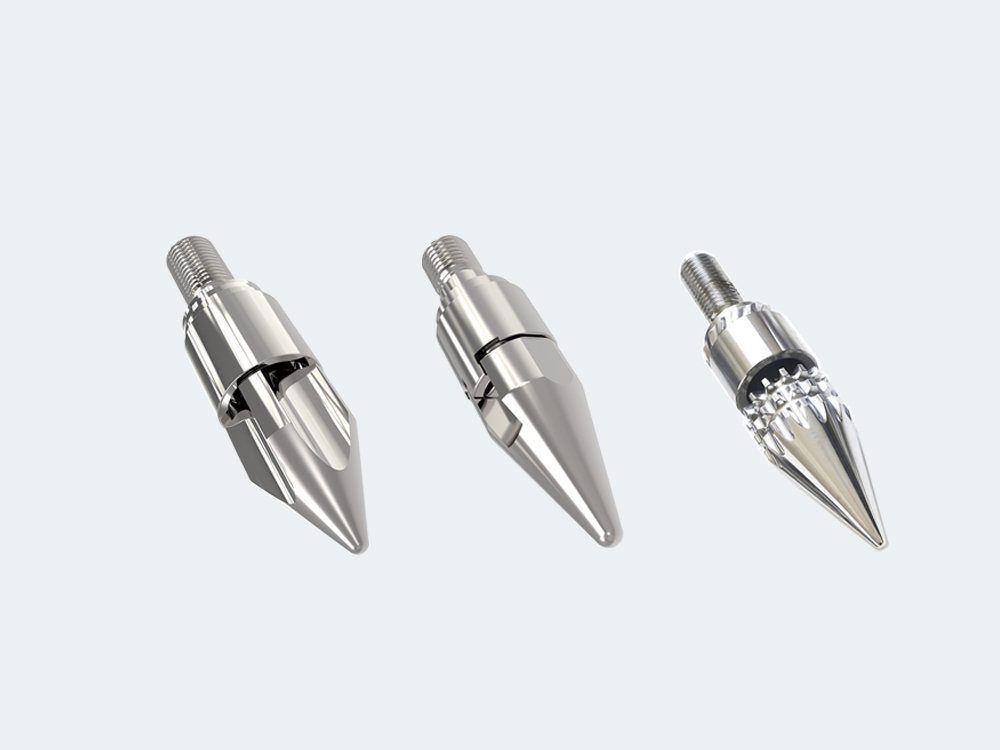
- 04Robust screw tips and check rings for reliable large-shot dosing.
- 05Reinforced, low-shear metering sections to protect part integrity.
Recommended Products
Applications / Materials
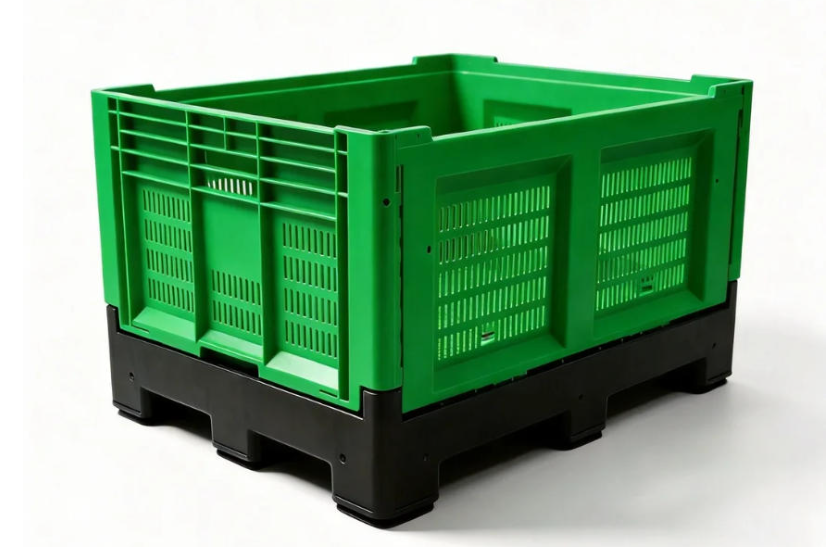
Returnable transport cratesWarehouse and logistics palletsBulk containers and IBC componentsHeavy-duty reusable packaging
Frequently Asked Questions
Large HDPE/PP shots, high regrind content and mineral or glass fillers abrade screw flights and barrel bore rapidly. Wear-clad (HVOF / tungsten carbide) screws and bimetallic barrels extend service life.
Size the screw to the shot and recovery time, use a robust screw tip and check ring for reliable large-shot dosing, and maintain barrel bore tolerance to keep packing pressure stable.
Machine make and model, shot weight, resin grade and regrind ratio, filler content, cycle time target, and the dimensions or drawing of the existing component.