Extrusion Single Screw
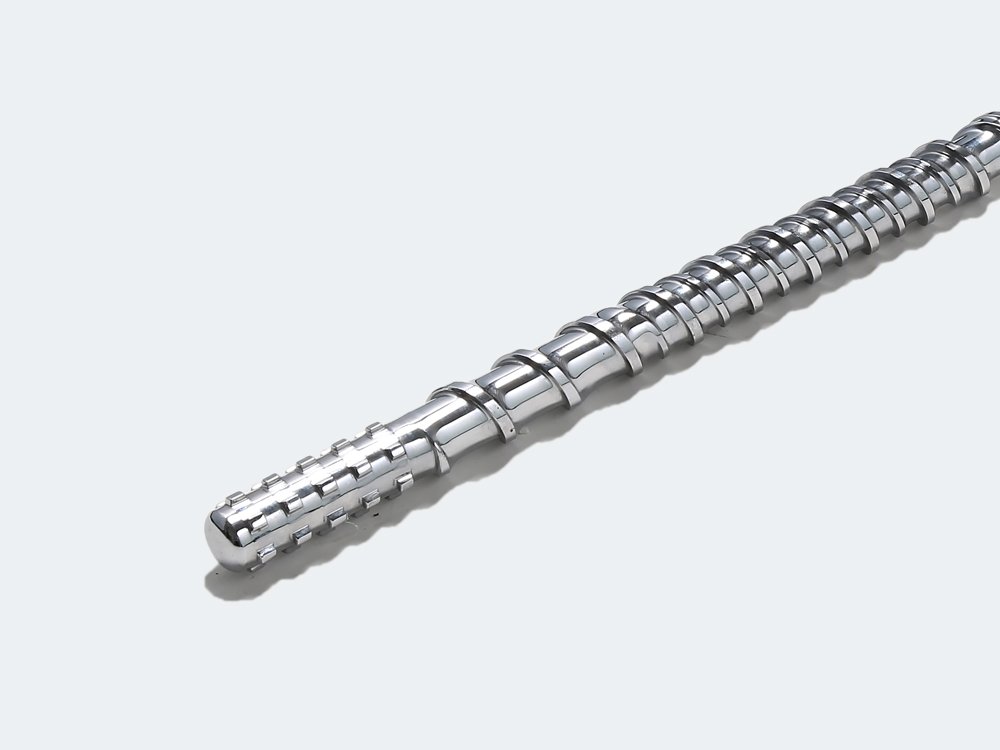
Extrusion single screws are built in barrier, mixing and metering geometries for stable output across continuous extrusion lines. With nitrided, PTA bimetallic or hardened flights and chromed or PVD surfaces, they serve pipe, film, profile and pelletizing applications and can be fully armored by PTA welding.
Technical data
| Name | Extrusion Single Screw |
|---|---|
| Material | 38CrMoAlA, SKD61, D2, DC53, C276 |
| Application | Pipe, Film, Profile, Pelletizing |
| Treatment | Nitrided, PTA Bimetallic, Hardened |
| Surface Treatment | Chromed, PVD |
| Manufacturing | Drawing or Sample Based |
| Screw Dia. | 1:28 | 1:33 | 1:38 | |||
|---|---|---|---|---|---|---|
| Speed (rpm) | Output (kg/h) | Speed (rpm) | Output (kg/h) | Speed (rpm) | Output (kg/h) | |
| Φ45 | ~70 | 50 | ~120 | 80-120 | ~150 | 120-180 |
| Φ60 | ~70 | 100 | ~120 | 180-250 | ~150 | 300-350 |
| Φ75 | ~70 | 160 | ~120 | 300-400 | ~150 | 400-500 |
| Φ90 | ~70 | 250 | ~120 | 400-500 | ~150 | 600-700 |
| Φ120 | ~70 | 350 | ~120 | 700-800 | ~150 | 800-1000 |
| Φ150 | ~70 | 500 | ~120 | 1000-1200 | ~150 | 1200-1500 |
Engineering highlights
- Profile standard or mixing type according to application
- Flight fully armored by PTA bimetallic welding
- Decades of years for profession design proposal
Frequently Asked Questions
A single screw transports, compresses, melts, and meters polymer through different screw sections. Its geometry determines how efficiently material is processed.
The polymer, output requirement, screw diameter, L/D ratio, compression ratio, processing temperature, and additives should be considered when selecting the screw design.
High-output extrusion requires a screw geometry that provides efficient conveying and melting while maintaining suitable pressure and melt temperature. The optimal design depends on the polymer and extrusion process.
Yes. ROOTIER can manufacture extrusion screws according to machine dimensions, material requirements, output targets, and customer drawings.