Injection Screw Tip
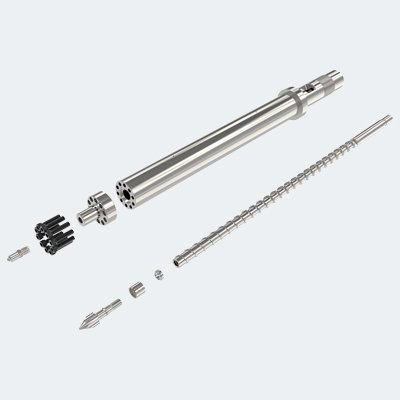
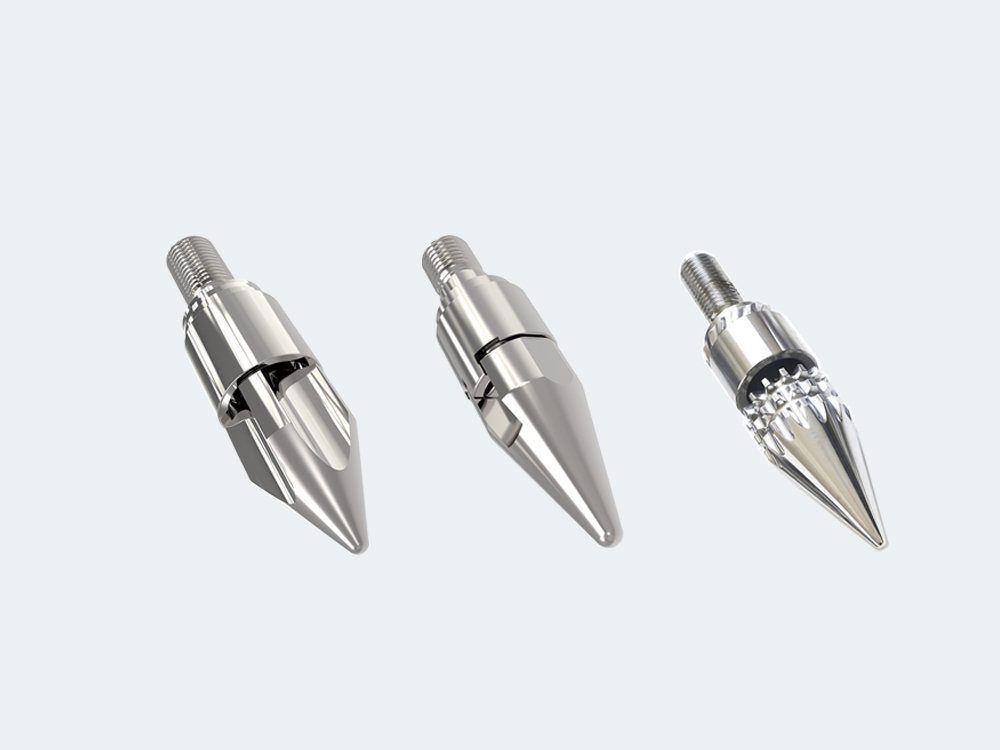
Injection screw tips and non-return valve assemblies provide consistent shot repeatability. Available in rotate and non-rotate types with bimetallic or PVD surface treatment, they are held in massive stock for fast delivery and can be armored for longer service time.
Technical data
| Name | Injection Screw Tip Set, Ring Plunger |
|---|---|
| Material | SKD61, D2, SKH55, M390 |
| Treatment | Bimetallic, PVD |
| Type | Rotate Type, Non-rotate Type |
| Manufacturing | Drawing or Sample Based |
Surface Treatment
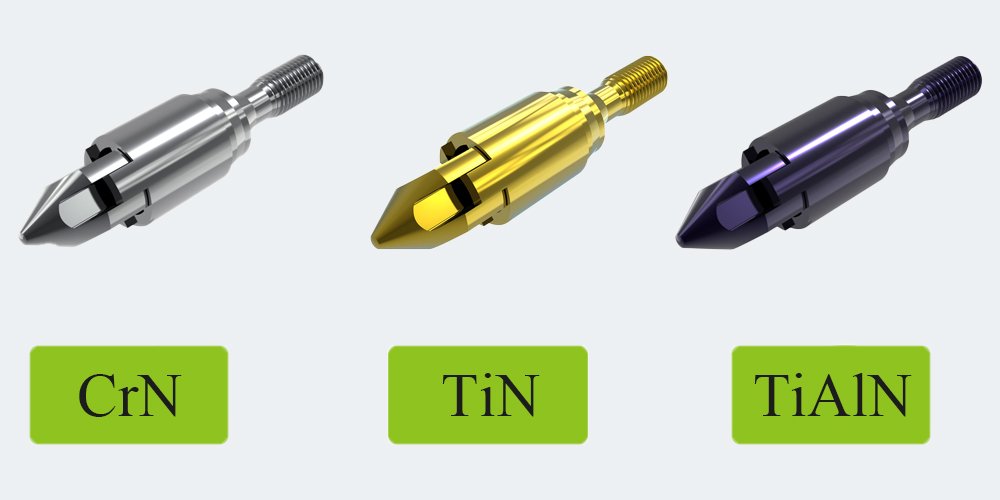
| PVD Type | TiN | CrN | TiAlN |
|---|---|---|---|
| Micro-hardness | 2000-2200HV | 1800-2000HV | 2800-3000HV |
| Thickness | 2-5μm | 2-5μm | 2-5μm |
| Friction Coefficient | 0.4 | 0.45 | 0.35 |
| Max. Temp. | 600° | 700° | 800° |
Engineering highlights
- Massive Stock for Fast Delivery
- Optimized design for better flow
- Screw tip bimetallic armored for longer service time
Frequently Asked Questions
The screw tip forms part of the screw check valve assembly and helps control polymer flow during plasticizing and injection.
Wear in the screw tip or check ring assembly can allow excessive backflow of molten plastic, potentially causing inconsistent shot size, pressure loss, and unstable molding performance.
The screw tip must match the screw dimensions, check valve design, machine specifications, material characteristics, and required injection performance.
Yes. ROOTIER can manufacture screw tips and related check valve components according to machine specifications and customer drawings.