Problem
Melt drools from the nozzle during mould open, contaminating the gate area, wasting material and forcing extra cleaning cycles that slow production.
Typical Causes
- 01Inadequate nozzle shutoff on low-viscosity or high-temperature resins.
- 02Excessive melt temperature reducing melt viscosity.
- 03Residual pressure in the barrel after injection.
- 04Worn nozzle seat or tip that no longer seals cleanly.
- 05Insufficient decompression (suck-back) after holding.
Technical Challenges
- Achieving clean shutoff without freezing off the nozzle.
- Matching shutoff mechanism to the resin and temperature window.
- Keeping cycle speed while preventing drool.
- Avoiding stringing at the same time as drool.
Rootier's Technical Solutions
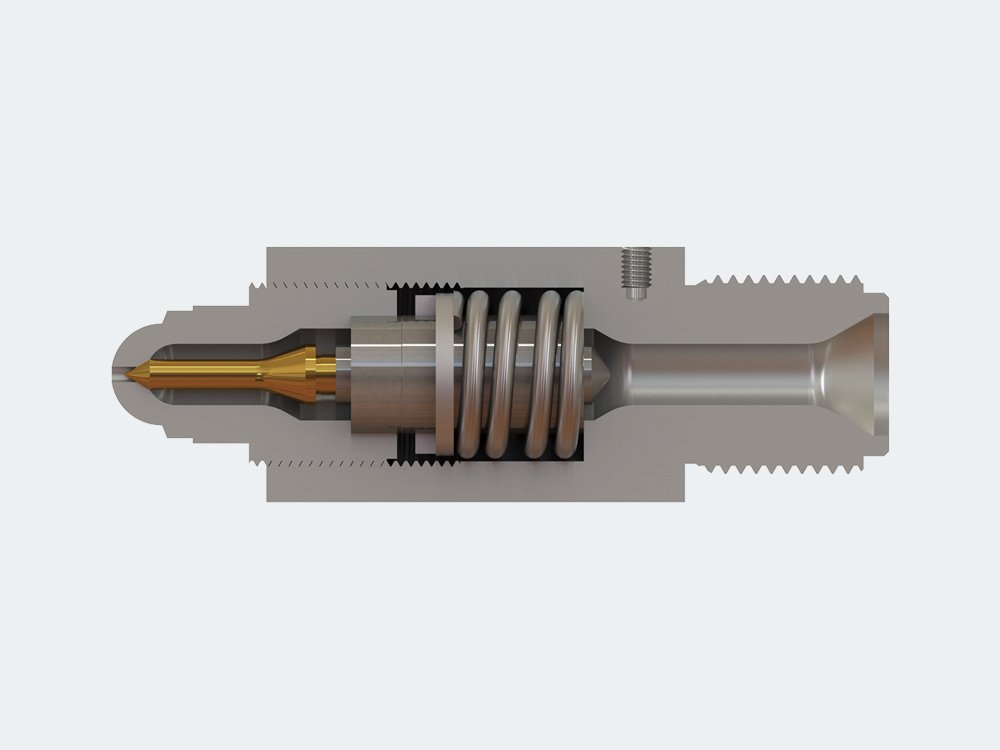
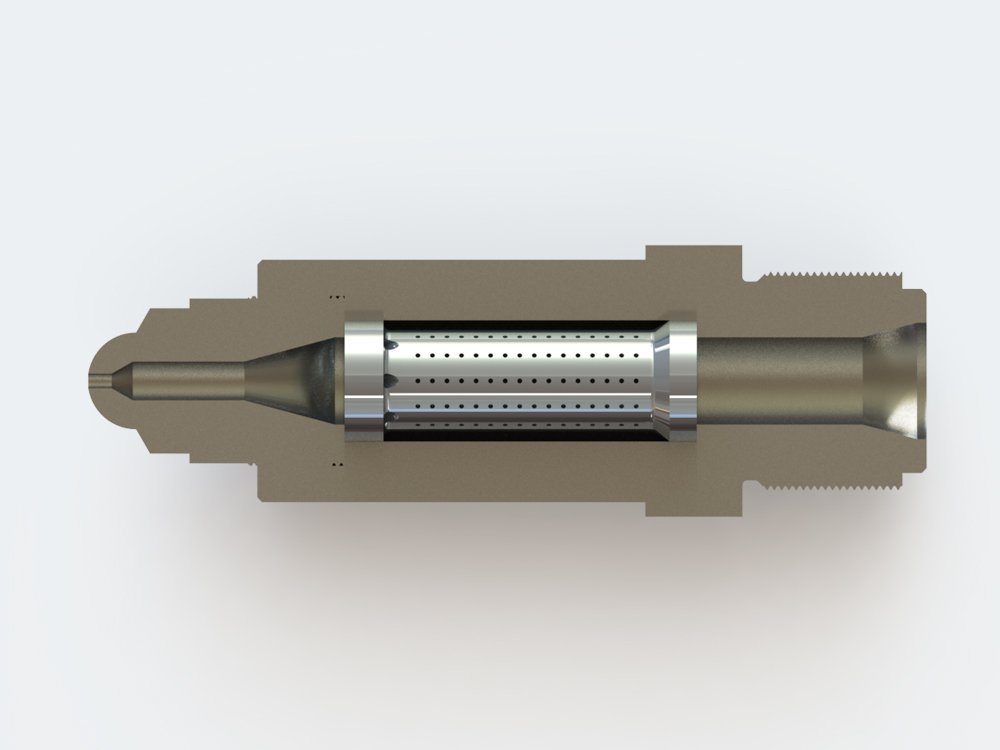
- 01Spring shutoff nozzles for simple, reliable melt blocking.
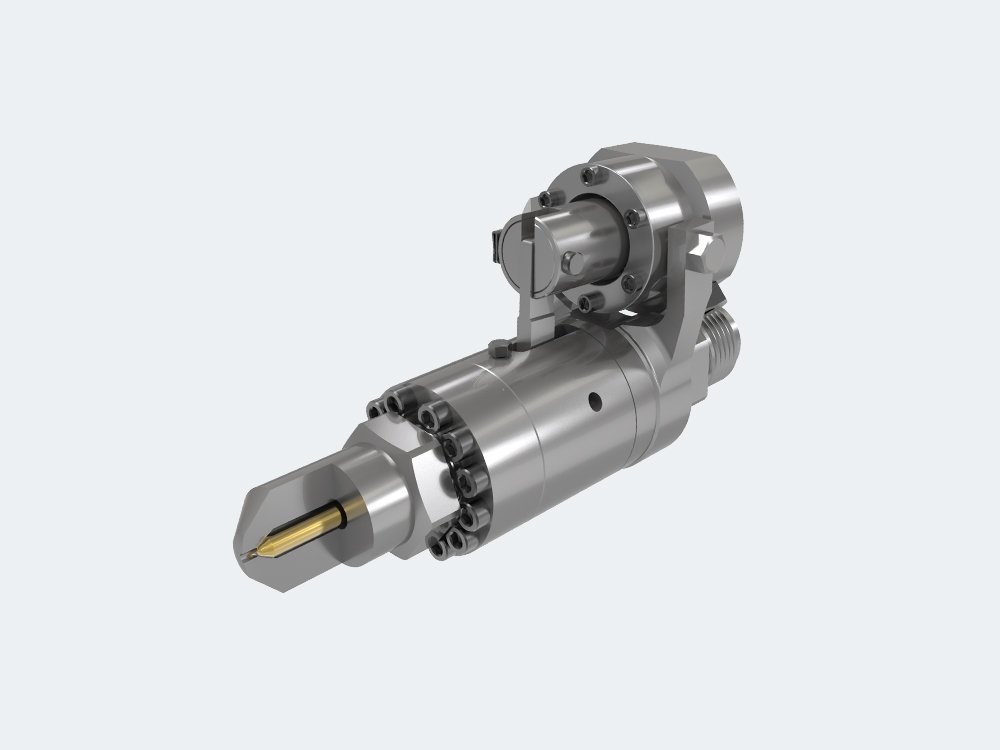
- 02Needle shutoff nozzles for positive, repeatable shutoff at high pressure.
- 03Piston shutoff nozzles for clean, synchronised melt control.
- 04Optimised nozzle tip geometry and surface finish to reduce adhesion.
- 05Guidance on decompression and temperature settings to complement the shutoff.
Recommended Products
Applications / Materials
Engineering plasticsLow-viscosity and high-flow resinsHot-runner and multi-cavity systemsPrecision and cosmetic moulding
Frequently Asked Questions
It depends on the resin and pressure. Spring shutoff nozzles suit simple cases, needle shutoff nozzles give positive sealing at high pressure, and piston shutoff nozzles offer synchronised melt control.
Excessive melt temperature, residual barrel pressure, a worn nozzle seat, or insufficient decompression can all cause drool. ROOTIER can match the nozzle and tip to your process window.
Yes. ROOTIER manufactures spring, needle and piston shutoff nozzles to your machine connection, nozzle dimensions, material and processing requirements.